Profile Extruder
Single Screw Extruders
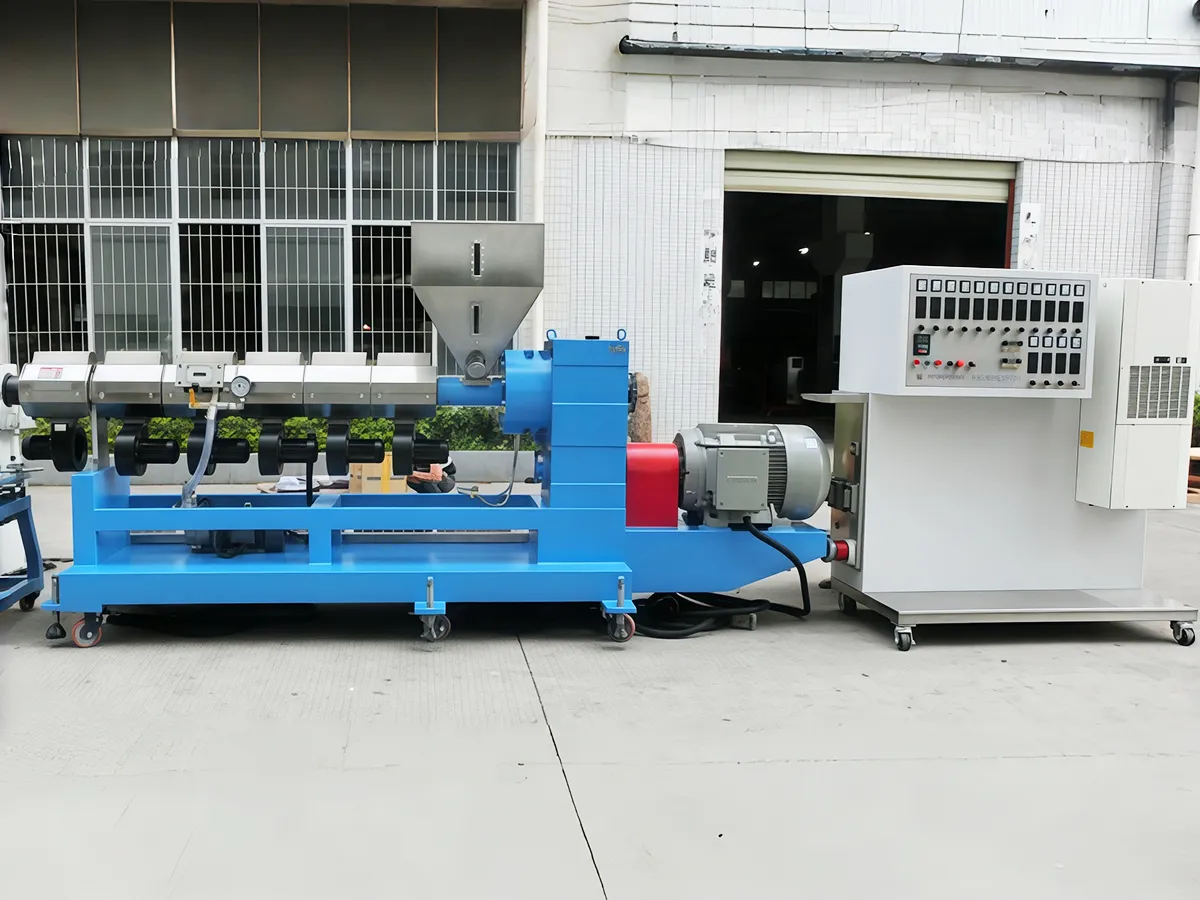
Profile extruders are used to produce continuous plastic sections which have the same cross-sectional shape over their whole length. The plastic pellets are first fed into the hopper, after which the motor drives a single screw through a gearbox in order to carry the material along the heated barrel. The heat from the extrusion barrel slowly melts the plastic as the screw mixes it and pushes it towards the profile die, the shape of the opening in the die deciding whether the final profile is solid, hollow, or of a custom shape. Once the profile has emerged from the die, sizing and cooling equipment determines its dimensions and helps to maintain its shape. The haul-off unit then draws the profile at a constant speed towards the cutting unit, which cuts each profile to the required length as the production process continues automatically.
PC, PMMA, PS, ABS, and other thermoplastics
- Plastic profiles for windows and doors
- Decorative profiles and trims
- Cable trunking and wiring ducts
- Custom plastic profiles with complex cross-sections
- Screw L/D Ratio: 25:1 / 28:1 / 33:1
- Approx. Extruder Dimensions (L × W × H): 2400 × 1250 × 1850 mm; actual dimensions vary according to the screw size and extruder configuration
- Capacity (kg/h): Varies according to the material, profile cross-section, and extruder configuration
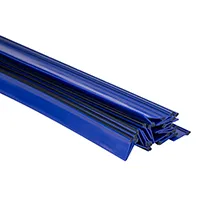 Brush Pile Seals (for Windows and Doors)
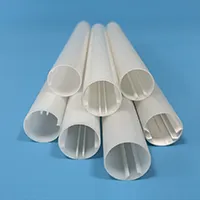 LED Tube Housings
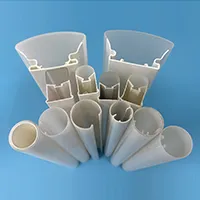 Polycarbonate Lighting Covers
- These profile extruders use a specially designed screw and mixing section, stable feeding, and separate temperature control for each barrel zone to melt and mix the plastic pellets evenly.
- The raw material is dried before it goes into the extruder, and as it melts, vacuum venting releases trapped gases while a streamlined internal flow path prevents buildup that could cause bubbles or specks (small visible material defects).
- Precise control of the feed rate, melt pressure, and temperature increases extrusion output while keeping the profile dimensions consistent.
- To support continuous production, our profile extruders have a high-torque drive and a wear-resistant screw and barrel, as well as separate cooling and lubrication systems that keep the main components operating smoothly over long periods.
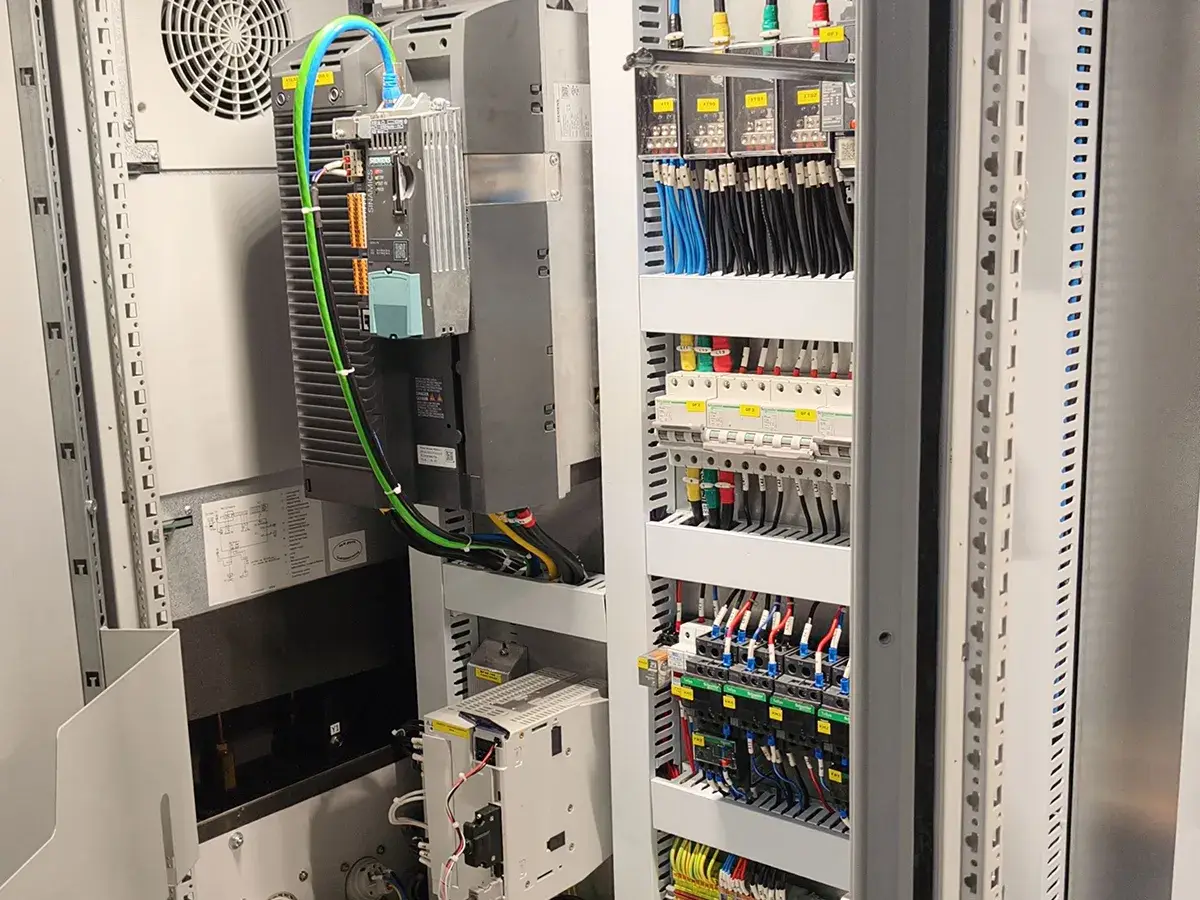
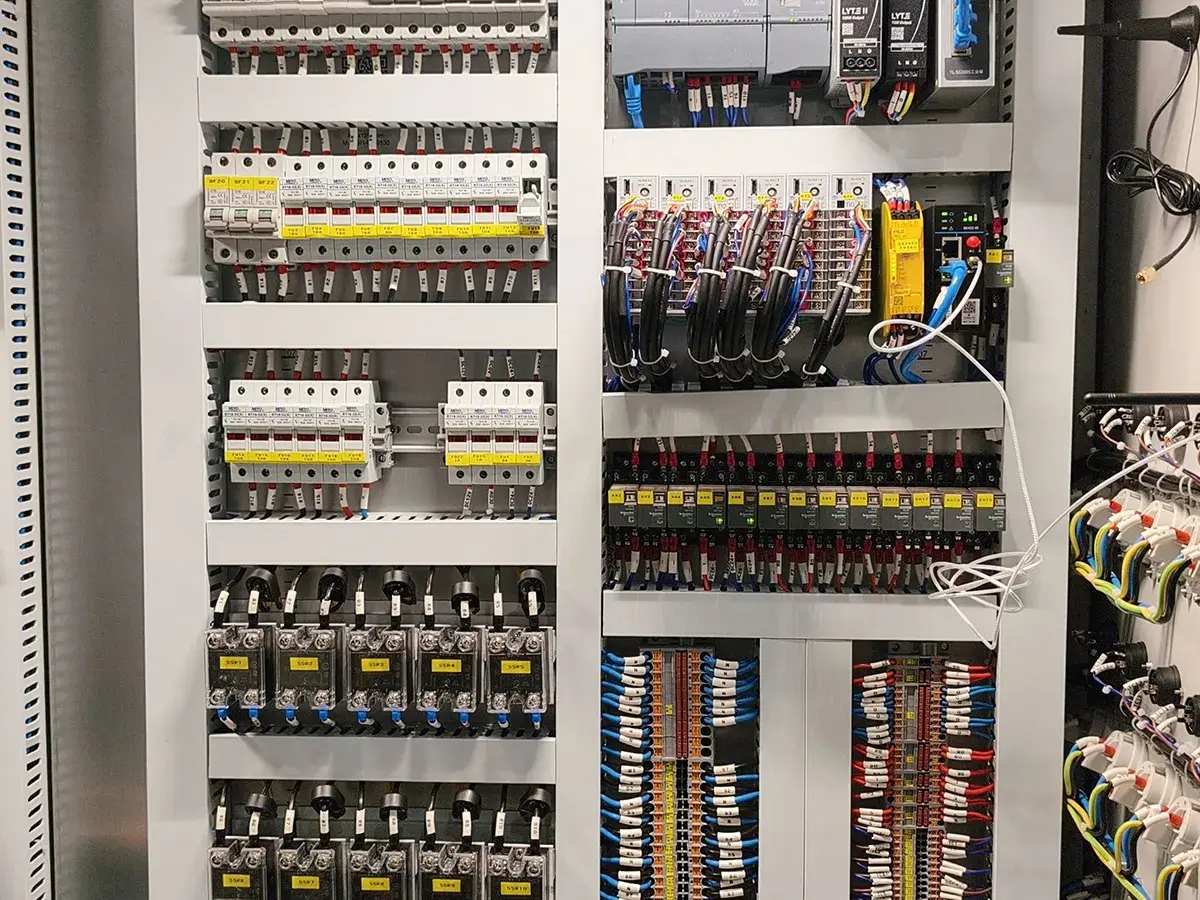
- The PLC and variable-frequency drives control the extruder speed and coordinate its operation with the downstream units for efficient, energy-saving, and automated production.
- Once the lighting-cover profiles leave the precision extrusion die, vacuum sizing keeps them round as they cool, while steady haul-off helps maintain consistent wall thickness and surface quality.