Precision Silicone Tubing Extrusion Line
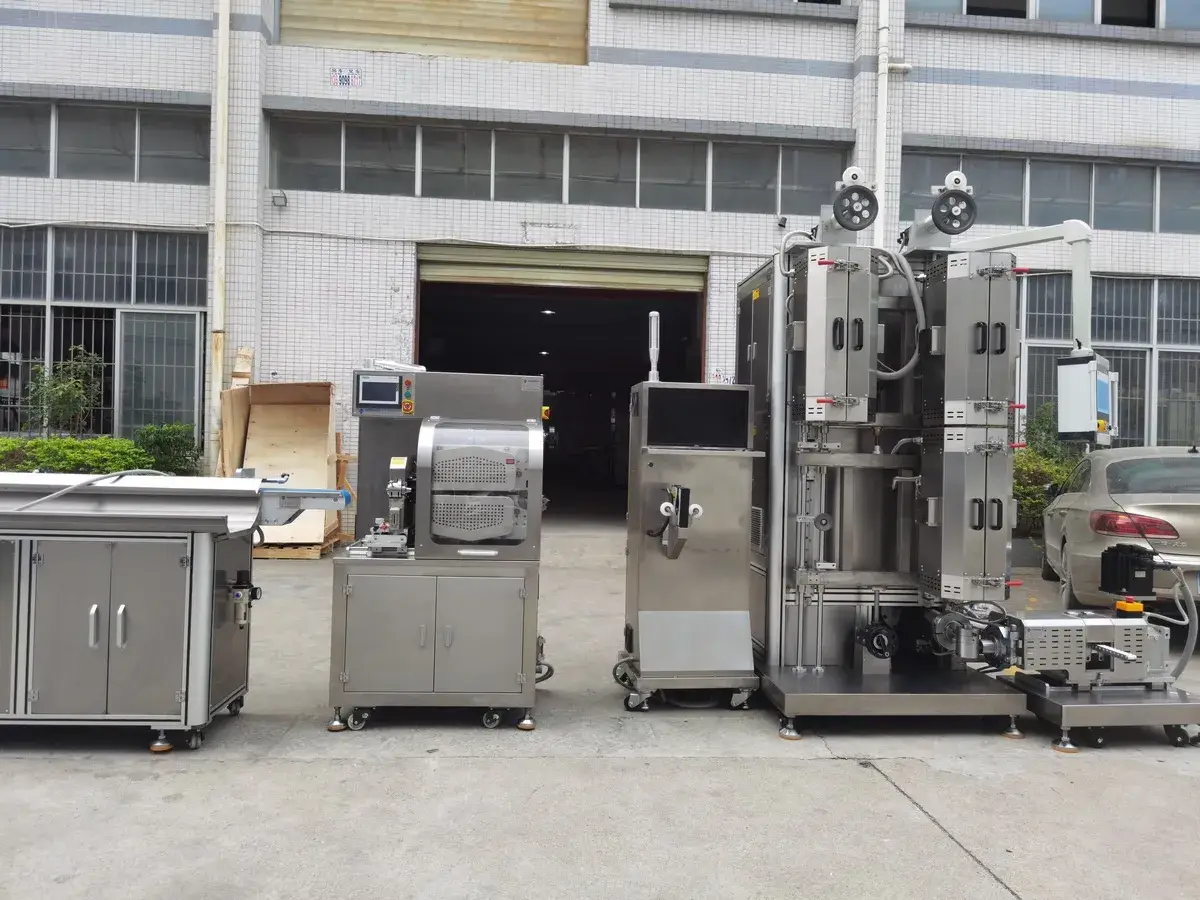
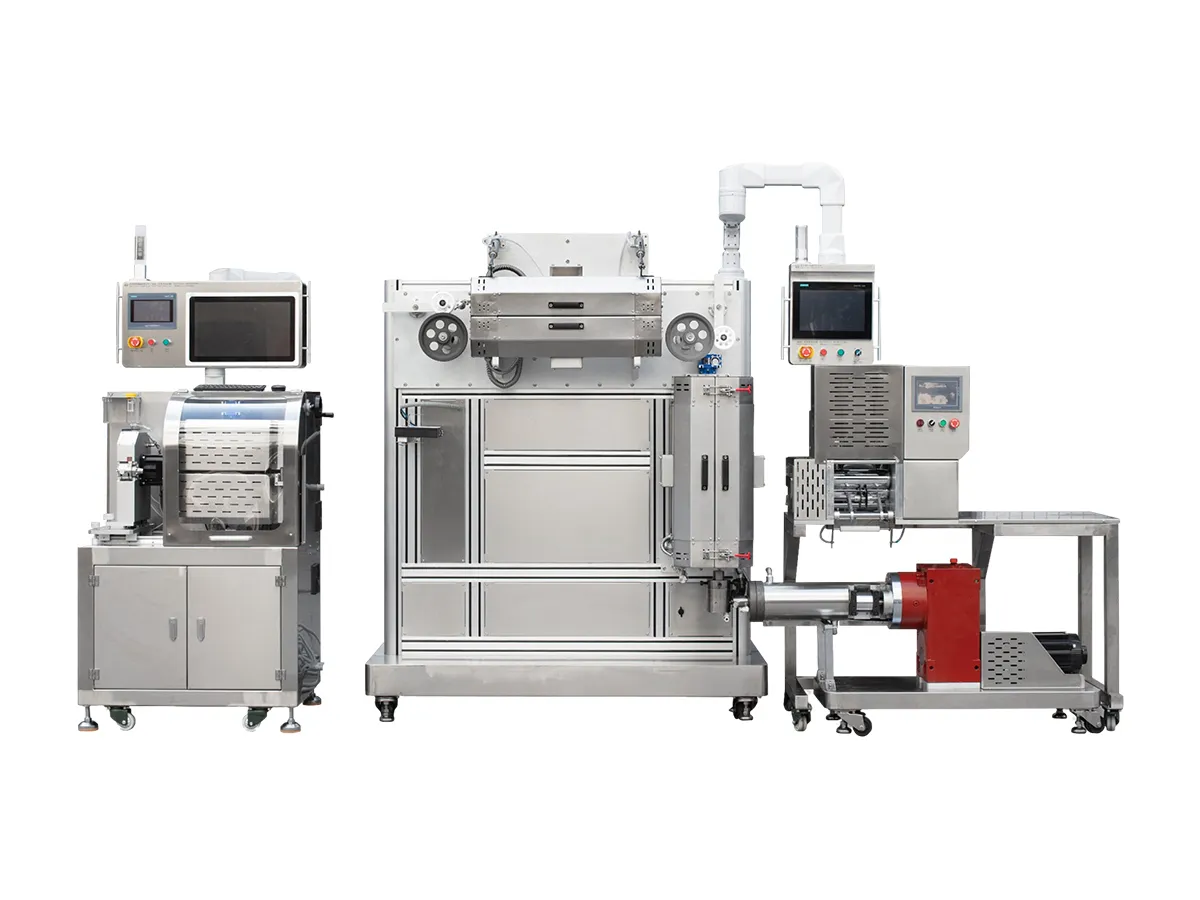
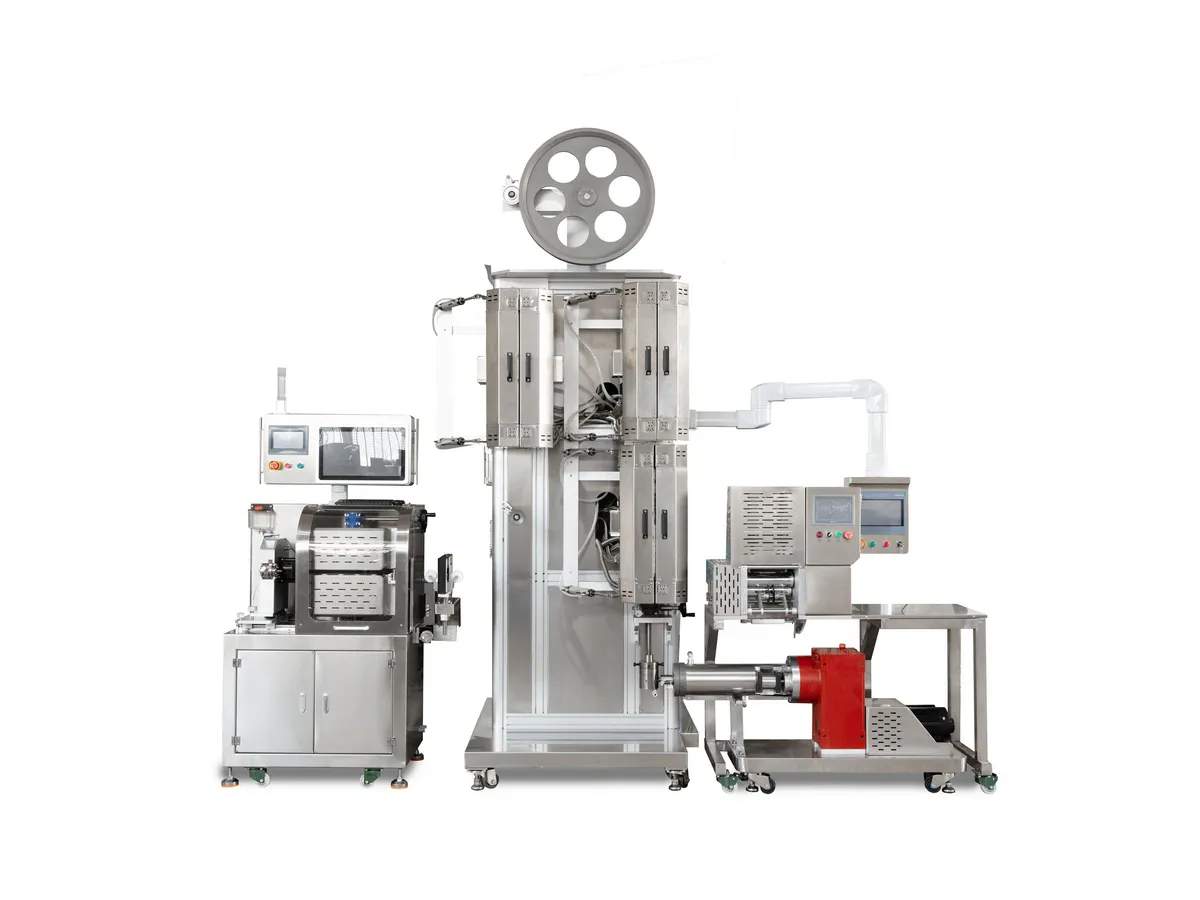
Medical-grade silicone tubing requires precise shaping and even curing to maintain consistent dimensions. Our precision silicone tubing extrusion lines combine a double-roller automatic feeder with a water-cooled single-screw extruder and die to process solid silicone and form the tube. Then it passes through a 0.6-meter ultra-high-temperature pre-curing oven and a vertical vulcanization oven before the haul-off and cutting unit pulls it forward and cuts it to length, with a conveyor completing the continuous automatic process.
Request a Quote
Watch Videos
Finished Product Samples
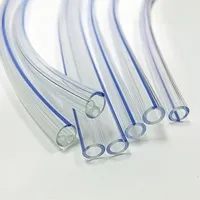 Color-Striped Silicone Tubing
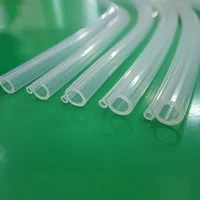 Bonded Silicone Tubing
Common Applications
| Extrusion Line Configuration | Medical Tubing Products |
| Vertical Precision Silicone Tubing Line for Micro and Ultra-Fine Tubes | High-value catheters for minimally invasive procedures, ultra-fine neurosurgical drainage tubes, and ophthalmic drainage tubes |
| Precision Medical Silicone Tubing Line for Standard and Long-Life Tubes | Peristaltic pump tubing for medical devices, extracorporeal circulation tubing, and ventilator circuit tubing |
| Dual-Color and Multi-Lumen Silicone Tubing Line for Complex Designs | Radiopaque or identification-striped drainage tubes, dual-lumen urinary catheters, and cross-shaped tubes that transition into a single lumen |
Technical Specifications
Based on 30 mm three-section vertical silicone tubing extrusion line.
| Screw Diameter | 30 mm |
| Screw L/D Ratio | 12:1 |
| Extrusion Direction | Vertically Upward |
| Max. Screw Speed | 60 rpm |
| Drive Power | 2 kW |
| Capacity | 5–10 kg/h |
| Overall Dimensions (L × W × H) | 3500 × 1500 × 7500 mm |
Features
- These multilayer medical tubing extrusion lines combine a precision extruder and die head with servo haul-off and inline diameter and wall thickness measurement to maintain the required outer/inner diameter, wall thickness, and concentricity.
- Several extruders can work with multilayer or coating die heads and tension controls to process different types of polymers, build multiple layers, or apply polymer coatings over metal cores.
- Equipped with an overcoating die that spreads the molten polymer evenly around the metal core, and maintains stable tubing dimensions, uniform wall thickness, and good concentricity. Preheating the core wire improves both physical adhesion and chemical bonding between the polymer and metal.
- The molten polymer is fed at a steady rate while monitoring its pressure and temperature in real time, then automatically adjust the extrusion output and haul-off speed to reduce dimensional variation and keep the coating thickness uniform and within tolerance.
- For products that need coating and sheathing, the core is accurately positioned and held at a steady tension as it passes through the precision die head. Then synchronized cooling stabilizes the new layer and reduces off-center or incomplete coating, delamination, and uneven wall thickness.
Main Components
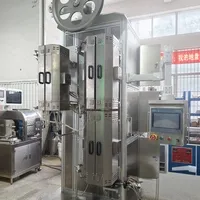 Vertical Multi-Section High-Temperature Silicone Extrusion and Vulcanization Unit
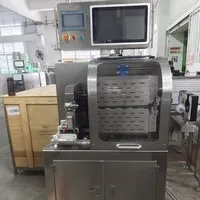 Haul-Off Unit with Diameter Measurement System
 Conveyor